Used Oil Re-refining
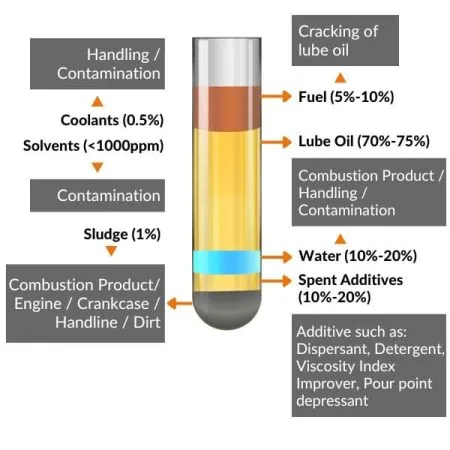
Sequoia’s process technology for re-refining used lubricating oils is based on distillation, adsorption and hydrotreating, recovering the 75% of valuable base oil still present in waste oil.
Learn more about Used Oil Re-refining
Sequoia Energy & Environment · Since 2006
We are experts in the design of process equipment for distillation, evaporation, hydrogenation, filtration and adsorption, as applied to recycling of liquids such as used oils, waste fuels and industrial wastes.
Who we are
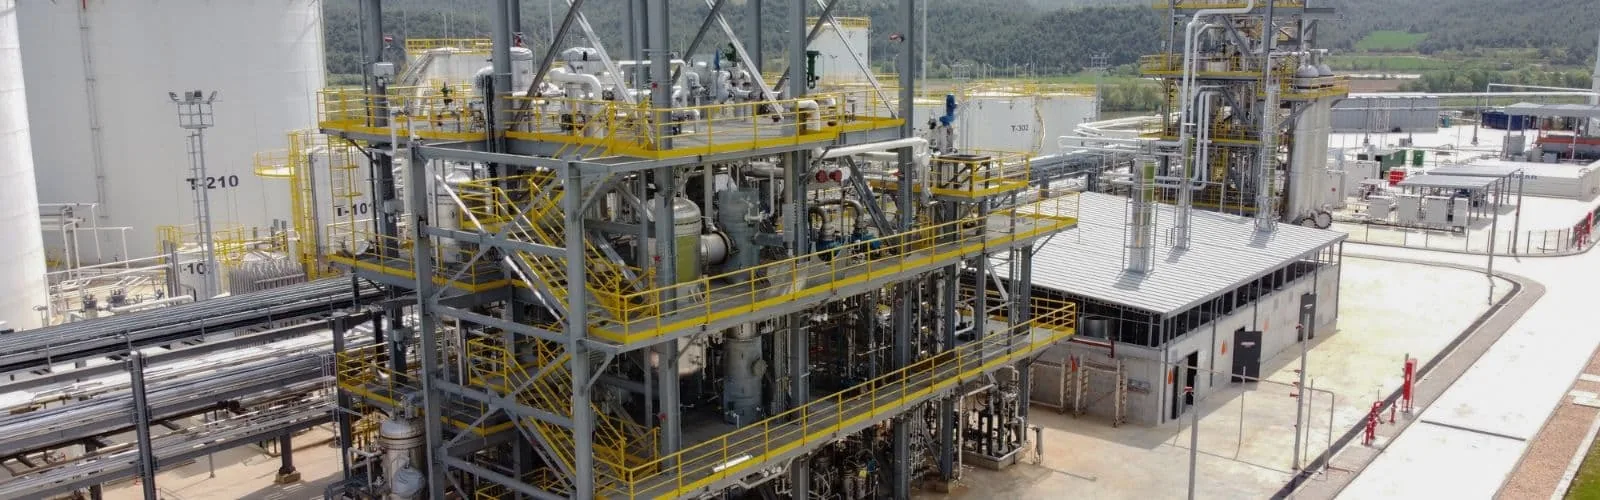
Since 2006, Sequoia has completed projects in the USA, Europe, Asia, South America and Australia. Sequoia delivers recycling and biofuel production solutions that provide a superior return on investment. With our state-of-the-art proprietary process technologies, we deliver value from project concept to start-up.
Our technologies are world class in robustness, ease of maintenance, energy efficiency, product quality and yields. Each plant is custom designed, and Sequoia supplies the equipment and modules and helps manage the project from conception to start-up.
Our expertise
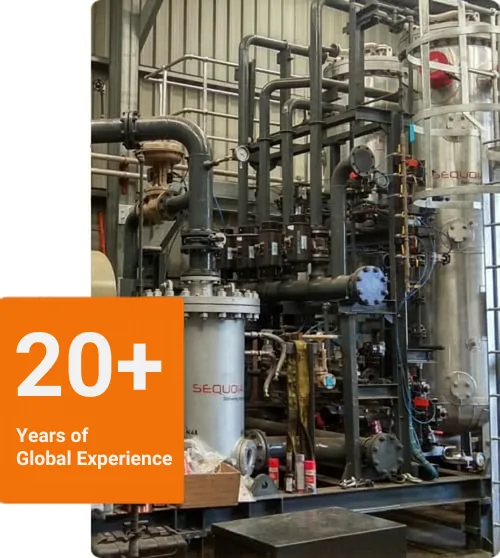
Proprietary combinations of distillation, evaporation, hydrogenation and adsorption, designed and supplied as complete, modular plants.
Sequoia’s process technology for re-refining used lubricating oils is based on distillation, adsorption and hydrotreating, recovering the 75% of valuable base oil still present in waste oil.
Learn more about Used Oil Re-refining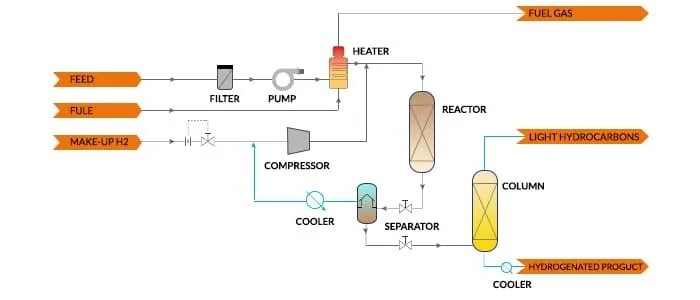
Hydrogenation plants that produce Group II or Group III base oil from solvent neutral base stocks, vacuum gas oils or used oils, renewable diesel (HDRD) from bio-feedstocks, and PCB-free transformer oil.
Learn more about Hydrogenation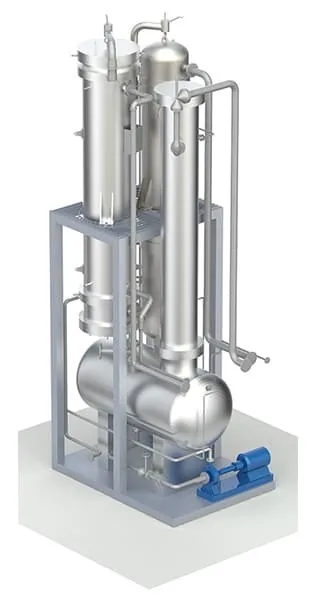
Sequoia’s coolant (antifreeze) recycling technology is based on vacuum distillation. It produces distilled water and more than 95% pure glycols from waste coolants.
Learn more about Antifreeze Recycling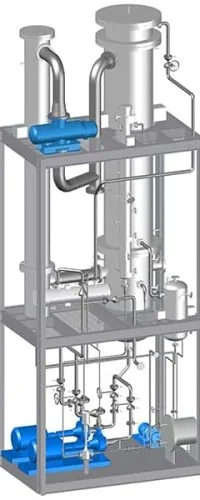
Sequoia’s evaporation technology incorporating vapor compression separates purer water from contaminants to produce boiler-feed quality water from high-TDS and hard-to-treat industrial wastewater.
Learn more about Wastewater Processing by Vapor Compression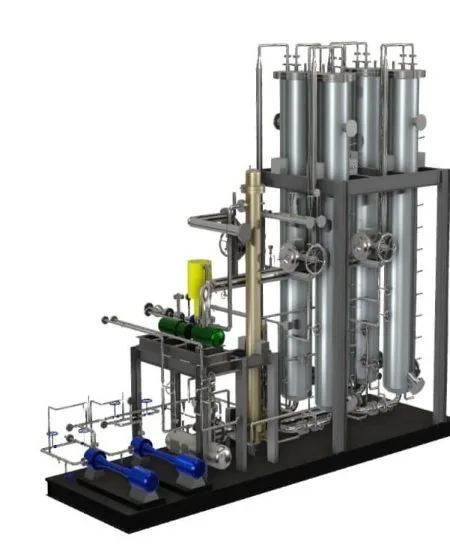
A two-step regenerative adsorption plant: oil is purified by adsorption on bauxite, and the saturated adsorbent is regenerated in-situ so it can be used again, improving colour, oxidation stability and viscosity index.
Learn more about Oil Purification by Bauxite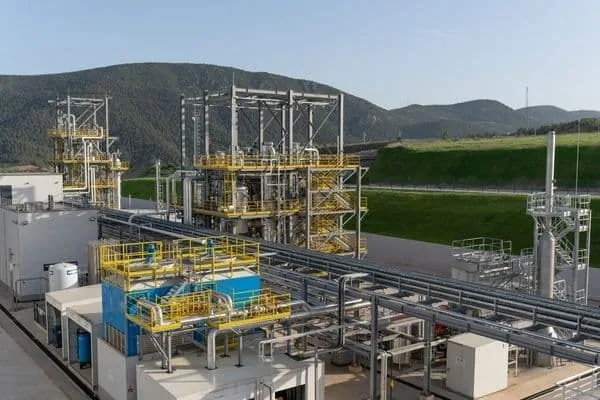
Hydrogenation combined with vacuum drying and filtration: the most complete process for recycling waste transformer oil into water-white, PCB-free insulating oil that meets OEM specifications.
Learn more about Transformer Oil Recycling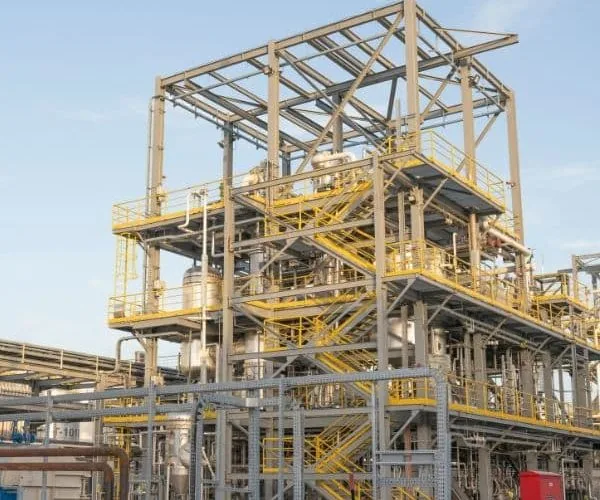
Heat-integrated evaporation equipment that removes free and emulsified water from waste fuel oils and recovers saleable diesel, leaving a residual heavy fuel that meets flash point specifications.
Learn more about Waste Fuel / MARPOL RecyclingCore technologies
Proprietary long-tube vertical evaporators with no moving parts and short-path wiped film evaporators.
Hydrotreating to Group II / III base oils, renewable diesel and PCB-free transformer oil.
Vacuum distillation that recovers lube base stocks, fuels and glycols at high yield.
Energy-efficient evaporation that produces boiler-feed quality water and enables ZLD.
How we deliver
Our engineering design centre and fabrication and assembly shop let us deliver projects on time and within budget, with process, mechanical, piping, electrical and instrumentation engineering carried out in-house.
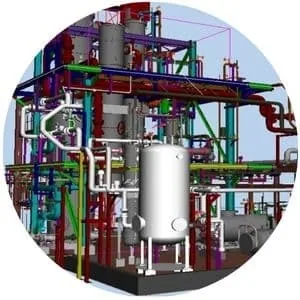
Custom process design using licensed process design, 3-D CAD piping and pressure vessel design software.
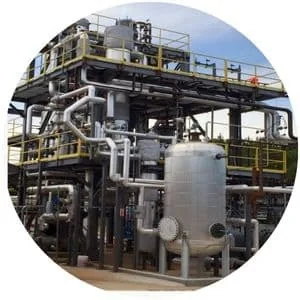
Equipment, modules, structural steel, piping, instruments and controls supplied under one contract.
Start-up support and years of operations support so the plant meets product specifications.
News and stories
Reference projects in Spain, Turkey, United States, United Kingdom, Uzbekistan and Argentina.
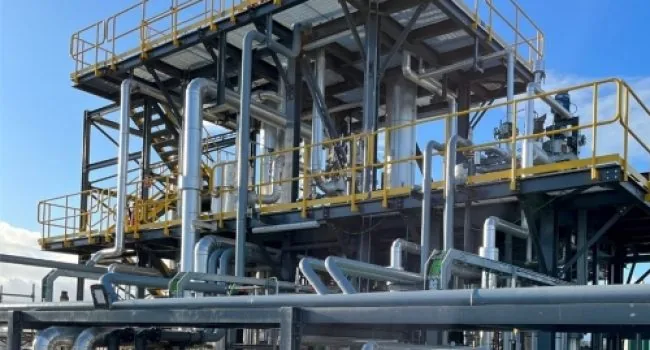 Galicia, Spain
A three-step vacuum distillation plant processing 50 tonnes per day of waste lubricating oil and fuels, producing distilled lube base stocks, fuels and a bitumen-grade residue with no solid or liquid waste.
Read the case study : Re-refining Plant by Sequoia Operational in Galicia, Spain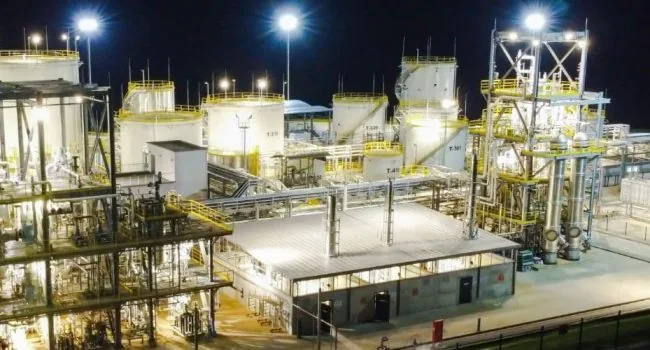 Osmaneli, Turkey
A vacuum distillation and hydrogenation re-refinery for Tayras that produces lube base oil exceeding API Group III specification, although it was designed for Group II.
Read the case study : Sequoia’s 60,000 Metric Tons Re-refining Plant Deployed in Osmaneli, Turkey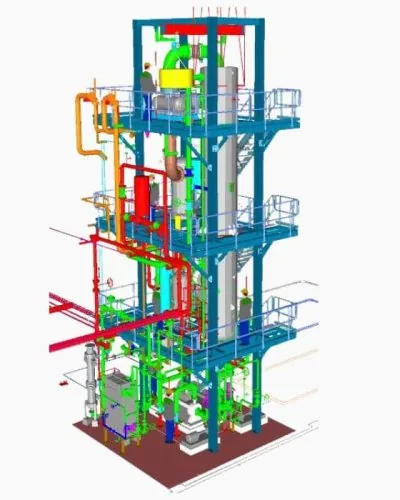 Nevada, United States
A vapor compression plant treating refinery wastewater with toxic organics, sulfides, phenols and glycol, recovering more than 75% as distilled water.
Read the case study : Wastewater Treatment Plant Using Vapor Compression is Operational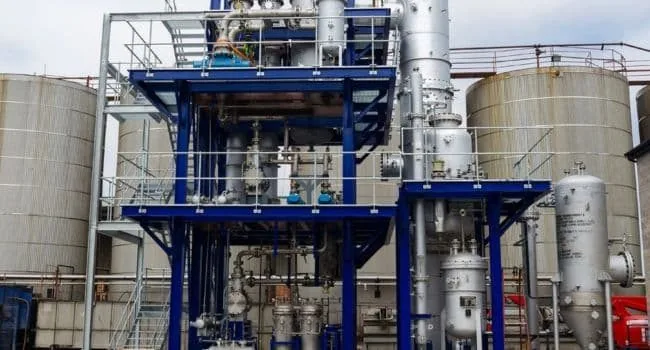 Merseyside, United Kingdom
A vacuum distillation plant at a port location that distills the lube oil fractions from 25,000 tonnes per year of waste motor oil, built in a narrow footprint under strict environmental permits.
Read the case study : Sequoia’s “Waste Oil to VGO” Distillation Process Operational in the UK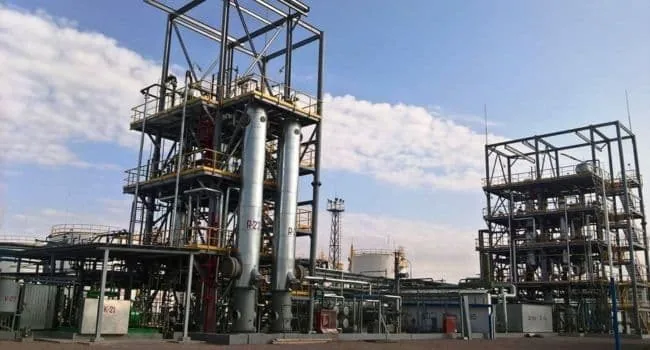 Uzbekistan, Uzbekistan
A complete re-refinery with vacuum distillation and hydrotreating that produces two grades of water-white Group II base oil from 45,000 tonnes per year of waste lubricating oil.
Read the case study : Sequoia Customer Uz-Prista Begins Production of Group II Base Oils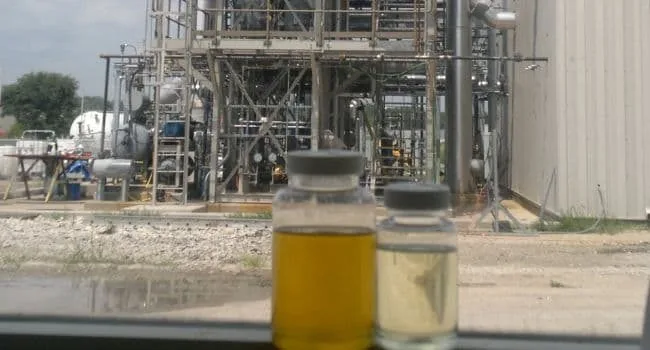 Kansas City, Kansas, United States
A naphthenic oil hydrotreater that turns waste transformer oil into PCB-free, water-white, low-sulfur insulating oil, with a thermal oxidizer for safe off-gas disposal.
Read the case study : Transformer Oil Recycling by Hydrotreating in Kansas CityTell us about your feedstock, capacity and location. Our engineers will advise on the right process technology, plant layout and expected economics.